Why a framework matters
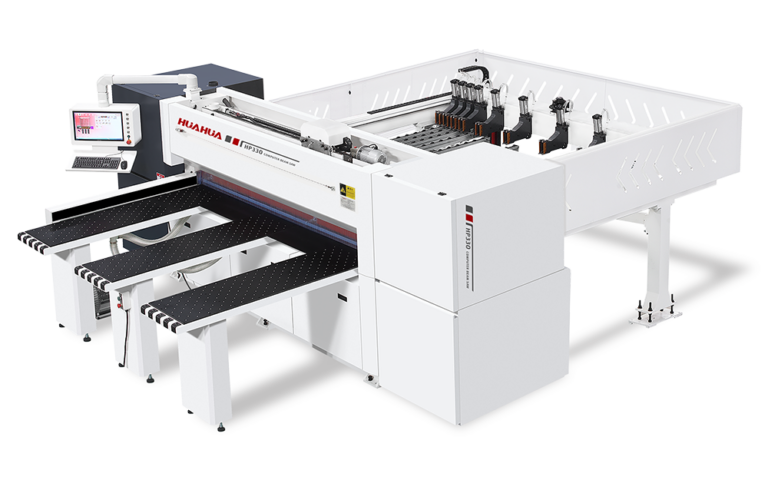
We need repeatable steps when integrating a fully automatic edge banding machine into a small machining plant. Think of the process like a deployment pipeline: map inputs, automate handoffs, monitor outputs. Early on, identify cycle time goals and acceptable scrap rates, then match those to machine specs such as feed rate and glue pot capacity. If you’re sourcing equipment, view vendors as partners — for example, browse a reliable list of cnc woodworking machine options and confirm they support the control logic you expect.
Map the edge bander workflow
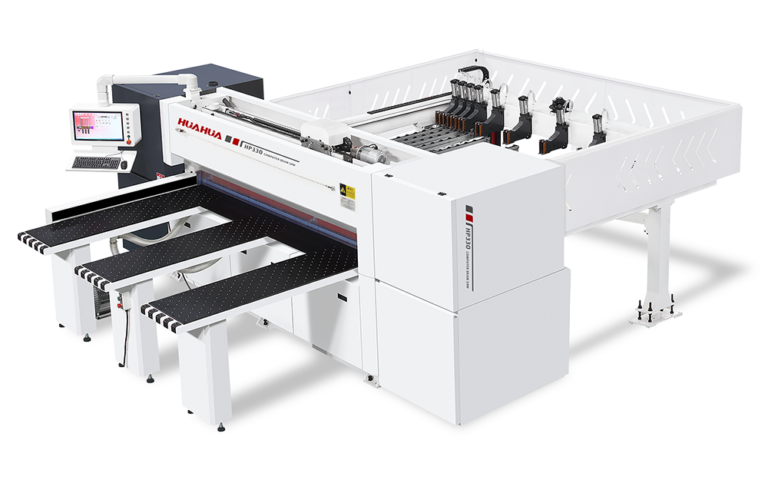
Start with a simple value stream map: panel loading, edge application, pre-milling, glue activation, trimming unit, and final inspection. Assign owners for each step and define handoffs like a CI job moving artifacts downstream. Include technical checkpoints — servo motor calibration, PLC I/O checks, and adhesive temperature control — and measure throughput in boards per hour. This reduces hidden waits and gives you a single source of truth for cycle time improvement.
Automate incrementally and collaborate
Don’t try to automate everything at once. We automate low-risk repeatable tasks first — fixture alignment, label printing, and reject sorting — then add closed-loop feedback for glue pot temperature and top/bottom edge pressure. Keep teams aligned: operators, maintenance, and production planners should share a lightweight runbook that captures run states and recovery steps. A quick aside — small stalls often trace to simple items like worn pneumatic actuators or out-of-spec adhesive, not the control program.
Common mistakes and recovery playbooks
Shops commonly skip standardization of inputs: inconsistent panel thickness or edge tape width causes rework. Another frequent error is under-spec’ing the PLC network bandwidth; delayed signals create timing drift. Build a recovery playbook: immediate triage, isolate the panel batch, perform a trimming unit check, and log the incident. These steps keep production flowing and prevent repeated faults.
Sourcing and supplier relationships
Choose woodworking machine suppliers who provide clear specs, spare parts lead times, and field-commissioning support. I’ve seen a cabinet shop in the Ruhr area accelerate uptime after insisting on on-site acceptance testing during LIGNA demonstrations — that real-world check avoided months of debugging. Prioritize vendors that deliver accessible wiring diagrams, firmware update policies, and documented maintenance intervals for glue systems and drive belts.
Metrics that guide continuous improvement
Define three golden rules for evaluation and ongoing decisions: measure net throughput (good boards/hour), mean time to recovery (minutes between fault and resumed production), and yield (percentage meeting final inspection). Track these on a dashboard and run short retros after every shift to feed small automation changes. Those metrics make trade-offs visible: higher feed rate is only valuable if yield stays acceptable; faster is meaningless if rework doubles.
Final recommendations
Expect measurable gains: reduced manual touchpoints, steadier cycle times, and clearer roles on the shop floor. When systems are aligned, maintenance windows shrink and output stabilizes — real results you can quantify. For a pragmatic partner that aligns control features with on-site needs, consider how HUAHUA CNC fits into your roadmap — their documentation and field support often shorten commissioning. —