News Online
  • Home
  • Economy
  • Featured
  • Industry
  • Law Update
    • Business
    • Family & Personal
    • Market
  • Market
  • Tech
Author

Brandon

Brandon

Tech

Selecting Appropriate RFID Tags: A Data-Driven Guide for Application-Specific Choice

by Brandon October 13, 2026
written by Brandon

Problem statement and empirical framing

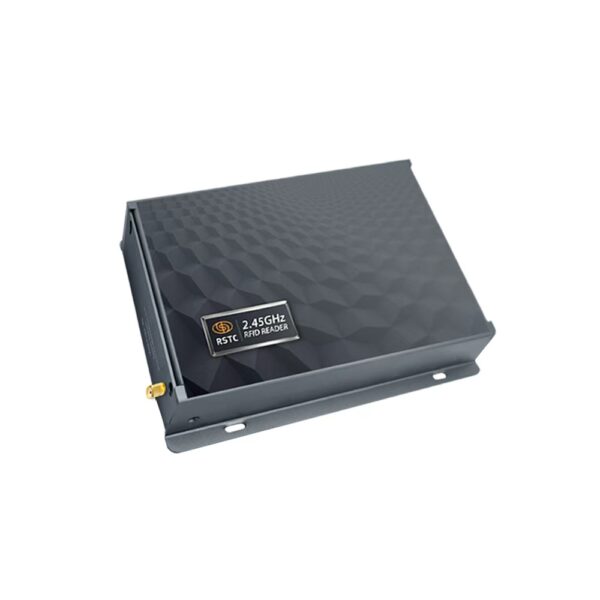
Many projects fail not because RFID is immature but because the tag choice does not match measurable system requirements; readers, antenna geometry and the physical environment together determine performance. Early in any procurement cycle one should quantify the target read distance distribution, throughput per read window and the expected tag population per interrogation zone, then confirm that candidate RFID Readers can meet those metrics. The remainder of this document uses objective metrics to translate operational requirements into tag specifications so that selection rests on data rather than anecdotes.

RFID Readers

Key measurable metrics to drive selection

Define and measure these parameters before specifying tags: read range (median and 95th percentile), read rate (successful reads per second per reader), orientation sensitivity (variation with tag angle), population density (tags per cubic metre), required memory (ID only versus user data), and ruggedness (temperature, chemical and abrasion tolerance). Complement those with regulatory constraints (regional UHF bands governed by FCC or ETSI) and operational KPIs such as acceptable miss-rate and latency. Each metric must have an acceptance threshold that a candidate tag must meet under a defined test protocol.

Tag technologies and their quantitative trade-offs

Compare families by their measurable properties. LF (125–134 kHz) yields high tolerance to liquids and proximity to metal but short range (centimetres) and low data rate; HF (13.56 MHz) suits short, controlled interactions (payments, access control) with moderate read reliability and standardised protocols (ISO 14443/15693). UHF (860–960 MHz) provides metres of read range and rapid population reads but is sensitive to polarization, tag placement, and regional regulatory power limits. Active tags add onboard power to extend range and enable sensors; they trade battery life and cost for ranges measured in tens to hundreds of metres. Choose by matching these quantified trade-offs to the previously defined KPIs.

Environmental factors that alter measured performance

Metal and water change the electromagnetic field and therefore the tag’s effective read range; quantify the degradation by measuring tag sensitivity in situ. Antenna polarization and multipath can both increase false reads and reduce reliability—measure polarization loss as a percentage of ideal read rate. Temperature and chemical exposure affect adhesive and encapsulation; perform accelerated ageing tests to estimate expected lifetime. Use controlled experiments to produce a matrix of read rate versus orientation, proximity to metal, and tag density; decisions must be grounded in those outputs.
RFID Readers

Standards, memory and security considerations

Specify protocol compatibility (for example, EPCglobal Class 1 Gen 2 for UHF deployments) as a hard requirement where interoperability is needed. Define minimum memory size for the use case and whether on-tag access control or cryptographic authentication is required; benchmark candidate tags for authentication latency and key storage model. Where privacy or chain-of-custody matters, include tests for secure read/write and tamper evidence as part of the acceptance criteria.

Common procurement and deployment mistakes

Purchasers often accept vendor-stated ranges without context, ignore reader–antenna matching, or under-test in representative environments. Cost-focused decisions sometimes select the cheapest tag type and then compensate with additional readers, raising total cost of ownership. Avoid specifying only nominal read distance; instead require performance tests under the busiest expected load. Also avoid overfitting a single pilot result—use multiple locations and representative materials to validate consistency.

Data-driven selection checklist

Follow this reproducible sequence: (1) quantify detection distance distribution, population density and acceptable miss-rate; (2) produce an environment test matrix (materials, temperature, humidity, orientation); (3) shortlist tag families (LF, HF, UHF passive, active) and candidate models that meet baseline specs; (4) run blinded lab and field tests measuring read rate, latency, orientation sensitivity and lifetime; (5) compare total cost of ownership including replacement rate and reader density; (6) require conformity to chosen standards and security tests; (7) run a staged pilot and collect KPI data before scale-up. Each step must produce numeric acceptance thresholds that the vendor must demonstrate.

Experience and authority anchored in practice

Field deployments demonstrate the necessity of this approach: large-scale retail rollouts that moved from ad hoc pilots to standardised, KPI-driven selection report measurable increases in inventory accuracy only after adopting structured testing. For example, European apparel chains that deployed RFID across stores reported conversions from inconsistent pilots to consistent store-level reads when selection criteria were enforced; those programs used readers and tag types chosen to meet defined read-rate and orientation metrics, and they evaluated performance with dedicated active rfid readers. Peer-reviewed operational studies and industry reports corroborate that empirical selection reduces deployment failures and lowers long-term cost.

Concluding synthesis

Selection of an RFID tag is an exercise in measurable constraints and trade-offs: define numeric performance goals, test candidate tags against those goals in representative conditions, and enforce standards and security requirements. When procurement follows these data-driven steps the chosen solution aligns with operational needs and matches available commercial offerings from established suppliers such as RSTC, which can supply components consistent with the specified metrics.
October 13, 2026 0 comments
0 FacebookTwitterPinterestEmail
Industry

Strategic Treatment Allocation: Maximizing Clinic Returns with High-Demand Skin Rejuvenation Programs

by Brandon July 16, 2026
written by Brandon

Why a framework matters for clinics and practitioners

When you run a dermatology or medical-aesthetics practice, the choice to expand or prioritise skin rejuvenation treatment offerings isn’t just clinical — it’s strategic. A clear framework helps you balance patient outcomes, equipment investment, and scheduling efficiency so that both clinical quality and revenue goals improve together. Taking a methodical approach reduces guesswork when deciding between investing in a fractional resurfacing laser, adding an IPL suite, or widening non-invasive modalities.

The four-pillar framework: Demand, Delivery, Dollars, and Durability

Organise decisions around four pillars that every clinic can measure and optimise.

1) Demand: Evaluate local patient needs, competition and seasonal trends. Many Toronto clinics, for example, saw rising demand for non-ablative procedures after 2020 as patients sought effective, low-downtime options.

2) Delivery: Match staffing, protocol development and device selection to expected case mix. Consider whether you need ablative or non-ablative platforms and whether fractional resurfacing or combined therapies will form standard packages.

3) Dollars: Calculate total cost of ownership — device acquisition, maintenance, disposables, and amortised training — and map revenue per treatment to utilisation rates.

4) Durability: Track outcomes such as patient retention, repeat bookings, and long-term satisfaction (neocollagenesis timelines), which determine whether treatments sustain centre profitability over years rather than months.

Patient pathways and procedure mix — designing for flow

Convert interest into repeatable visits by designing clear patient pathways: consult → staged treatment plan → follow-up and maintenance. Prioritise protocols that align with practice capacity. For example, layering IPL for pigment with a later session of fractionated laser can yield superior results but requires planning for staggered bookings and patient education on downtime. Use standardised intake forms that capture skin type, prior procedures, and expectations to reduce last-minute cancellations.

Capital allocation: selecting devices with an ROI mindset

Not all devices deliver equal returns. When evaluating purchases, perform a simple ROI model: estimate monthly billable hours, average revenue per session, and break-even months factoring in service contracts. Device features to weigh include laser wavelength versatility, pulse modulation, and footprint for clinic space. Renting or leasing can reduce up-front risk for higher-cost platforms; however, ownership typically lowers long-term cost per treatment for high-volume practices.

Pricing, scheduling and packaging strategies

Revenue rises when you combine sensible pricing with smart cadence. Offer tiered packages (single session, short course, maintenance) that reflect clinical reality — most facial skin rejuvenation treatments benefit from a series rather than a standalone visit. Implement dynamic scheduling blocks so that predictable procedures fill consistent slots, while shorter touch-ups use flexible openings. Track no-show rates and adjust deposit policies to protect revenue without creating patient friction.

Operational pitfalls to avoid

Common mistakes are predictable and preventable. Underestimating training time for staff on a new laser platform leads to slower throughput and patient dissatisfaction. Overpromising results without setting realistic expectations causes poor retention. And failing to document standard operating procedures for pre- and post-care increases complication risk. A practical fix is staged rollout: start with a pilot clinician and a limited treatment menu, collect outcomes, then scale — a small investment up front usually prevents larger problems later.

Measuring success: KPIs that matter

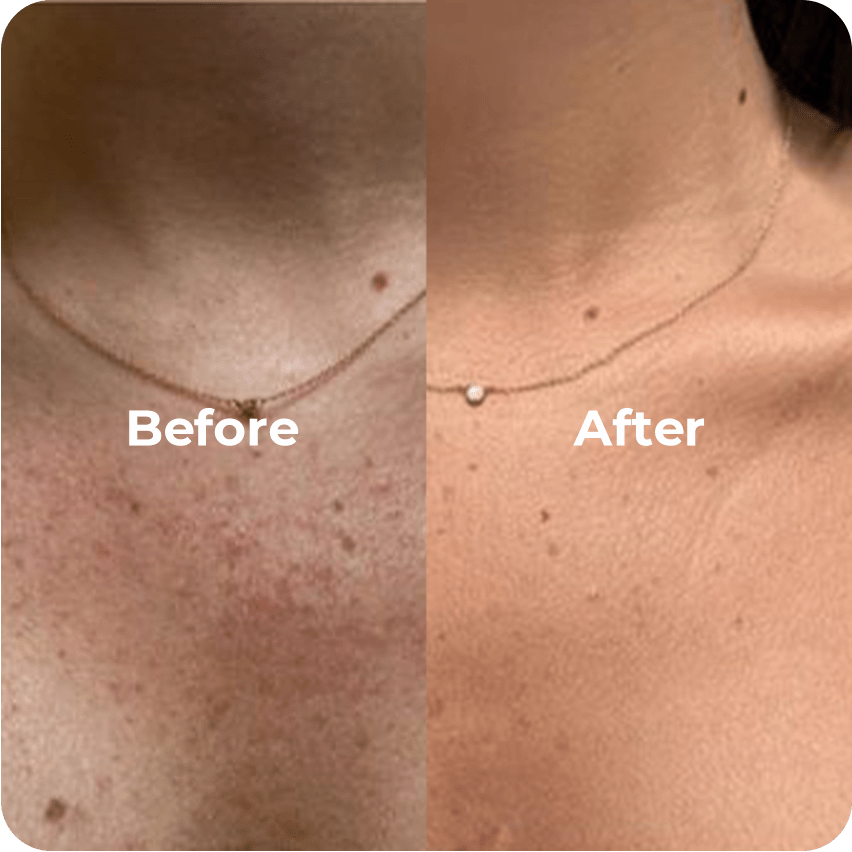
Track a concise set of KPIs weekly and monthly: utilisation rate (hours device was billable / available hours), average revenue per treatment, repeat-treatment rate (within 12 months), and complication/return visit rate. Combine these with patient-reported outcome measures and simple before/after photography to assess clinical durability. These metrics let you refine which procedures to promote and which to re-evaluate.

Alternatives and adjuncts worth considering

If device capital is a barrier, consider strategic partnerships — shared device arrangements with nearby clinics, mobile specialist days, or outsourcing advanced cases to a partnered centre. Adjunct offerings, such as topical cosmeceuticals or physician-led peels, can increase lifetime value per patient without heavy equipment costs. Finally, digital channels for education and booking lower friction to initial consultations.

Real-world anchor and ethical considerations

In practice — based on observations from multiple clinics in Ontario and public shifts post-COVID — demand trends have favoured low-downtime modalities that deliver visible improvement. Ethical practice means transparent consent, documented expected outcomes (especially when using terms like “rejuvenation” or “photorejuvenation”), and conservative marketing that reflects evidence-based results rather than hyperbole.

Summary and next steps

Deploy the four-pillar framework to align clinical needs with financial reality: assess local demand, define delivery workflows, model dollars carefully, and measure long-term durability. Start small, pilot responsibly, and scale what clearly shows clinical effectiveness and financial return. Tracking a short set of KPIs will keep strategy grounded in measurable outcomes.

Three golden rules for selecting and scaling skin rejuvenation services

1) Prioritise treatments with repeatable clinical outcomes and predictable utilisation — invest where throughput matches demand. 2) Protect margins by counting total cost of ownership, not just sticker price — include service plans and consumables. 3) Build patient pathways that set expectations and encourage series-based care; clear education converts first-timers into long-term patients.

These rules will help you choose wisely and scale confidently — and they explain why clinics that plan strategically often outperform peers. —

ENZOEYS.

July 16, 2026 0 comments
0 FacebookTwitterPinterestEmail
Tech

Resolving Peak-Demand Stress in Automotive Plants: The Practical Case for High C‑Rate Home Energy Storage

by Brandon April 1, 2026
written by Brandon

The immediate problem: why peak demand is urgent now

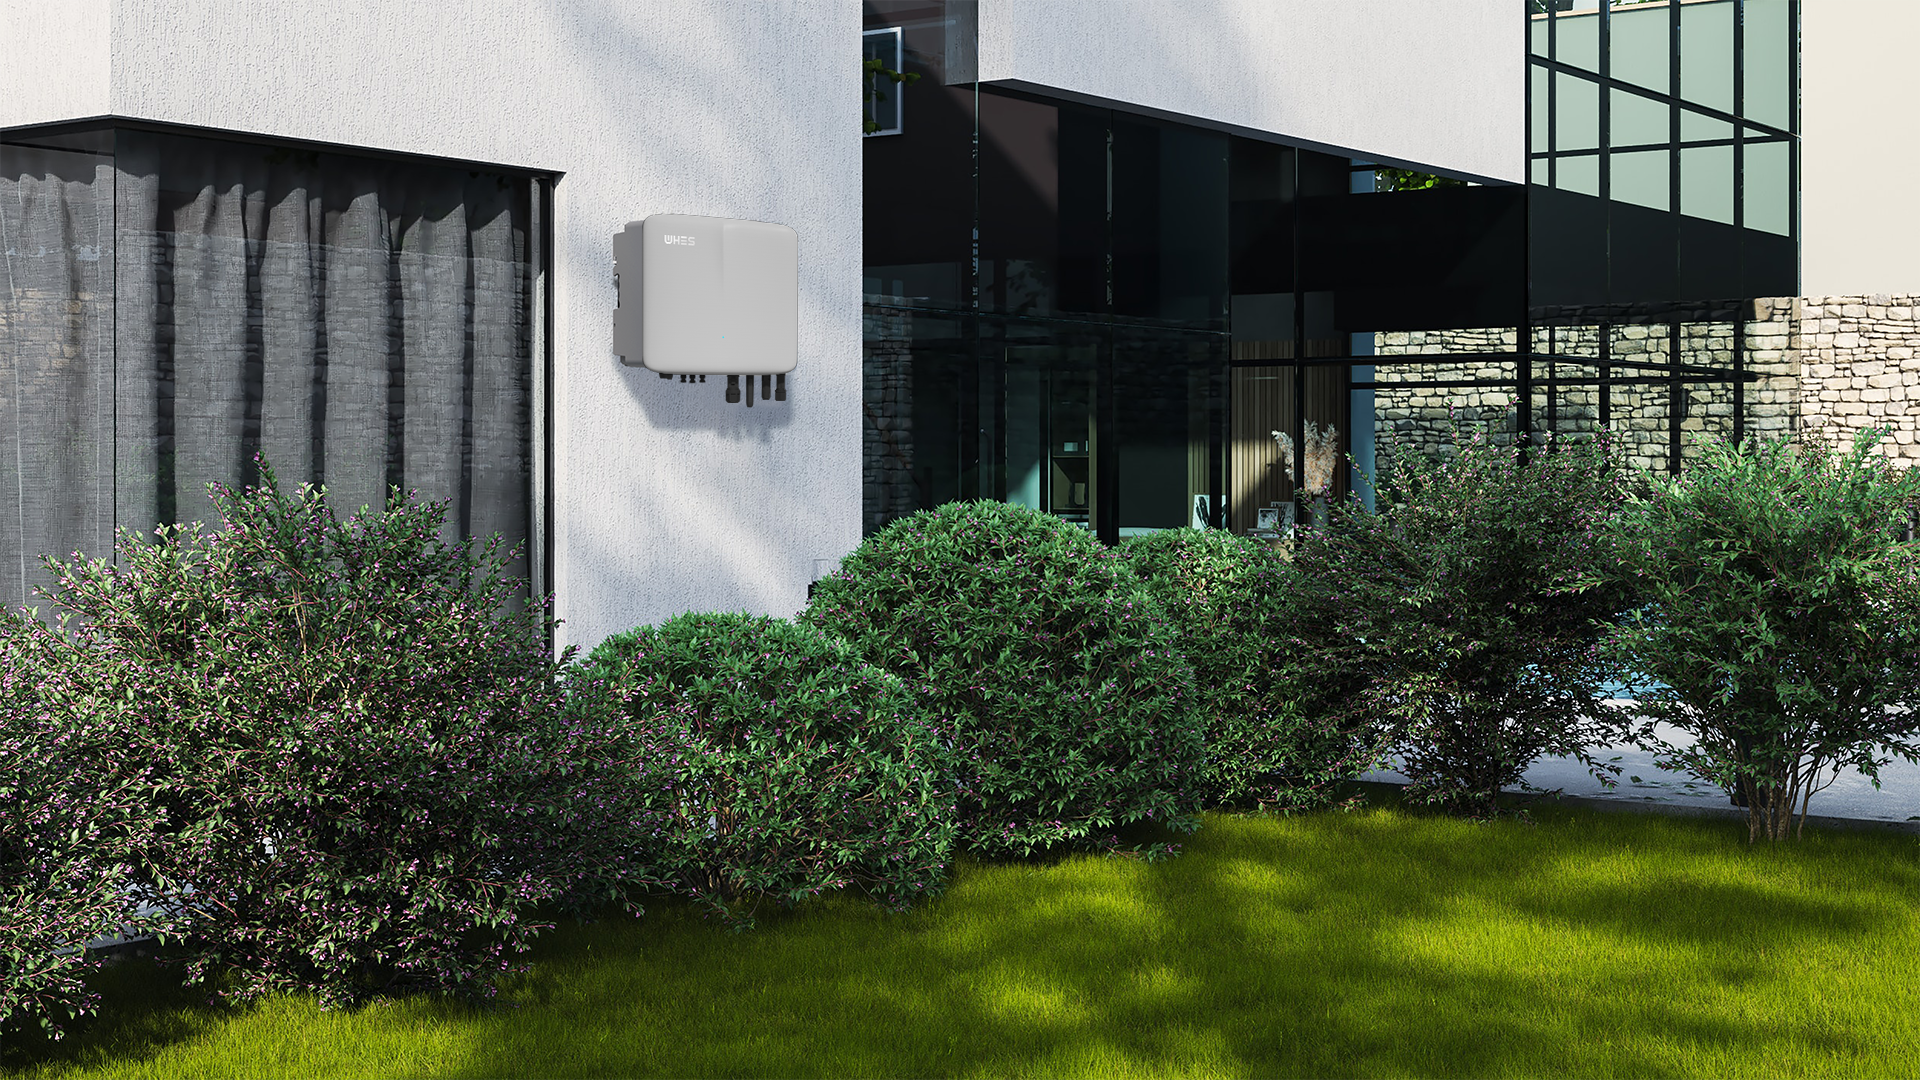
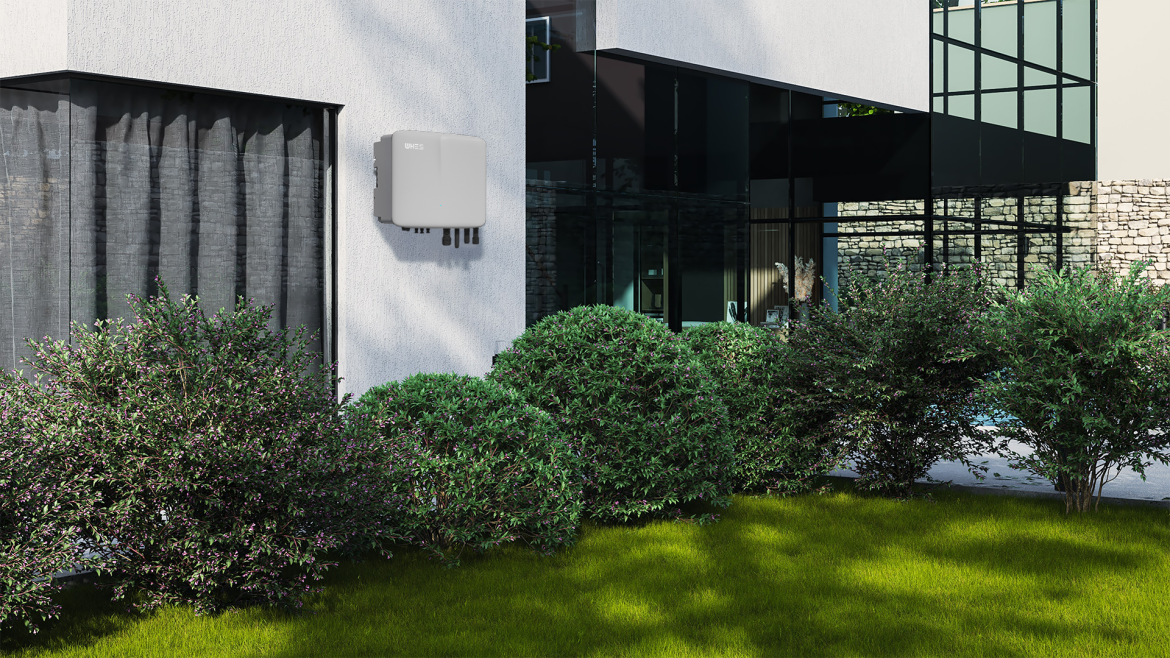
Many automotive factories are now confronted with rising peak-demand charges and tighter grid constraints that threaten production continuity and margins. When assembly lines and paint shops draw simultaneous power, utilities levy demand fees that can account for a large share of the monthly bill. One practical mitigation is installing local energy storage paired with smart power electronics — for example a three phase hybrid inverter — to perform controlled peak-shaving and ensure stable supply during transient loads. This problem-driven view asks not whether to adopt storage, but how to size, integrate, and operate it so that production reliability improves while costs fall.

three phase hybrid inverter

How peak loads form in automotive factories

Peak loads typically arise from concurrent high-power operations: spot welding banks, HVAC at shift changes, paint-bake ovens, and large motor starts. These short-duration events drive demand spikes that are billed differently from energy consumption. In addition, as factories electrify processes previously powered by gas, the magnitude and frequency of peaks can increase. It is therefore important to treat demand management as an operational discipline rather than a one-off capital project.

The role of high C-rate home energy storage in industrial settings

High C-rate storage provides rapid discharge capability, which is ideal for shaving short, sharp peaks without oversizing the battery bank. Such systems can supply motor inrush currents and support transient voltage sag, while preserving the main supply for sustained loads. Key performance considerations include inverter efficiency, state of charge (SoC) control, and ramp-rate capability. When paired with a grid-tie inverter and an intelligent energy management system, these storage units act as a fast-responding buffer between factory demand and utility supply.

Sizing and power electronics: where the 10 kW class fits

Sizing must reflect both peak power and usable energy. Many workshops find a modular approach practical: several high-C-rate battery modules coupled with appropriately rated inverters to handle three-phase loads. A common on-site component is a 10 kw 3 phase inverter, which can manage balanced three-phase outputs for small substations and microgrid segments. When selecting such equipment, pay attention to continuous vs. peak rating, harmonics handling, and protective relay coordination. Proper integration prevents unwanted tripping and ensures smooth handover between grid and battery during a peak event.

Implementation pitfalls and operational lessons

Practitioners often make two mistakes: underspecifying discharge power for short-duration peaks and neglecting communications between the storage controller and factory energy-management systems. It is also common to trust lab-rated inverter efficiency without verifying real-world losses under motor-start conditions. A practical remedy is to run site-specific load profiles for a week and emulate worst-case start sequences in a controlled test. — This reveals whether the chosen C-rate and inverter combination truly meets demand.

Real-world anchor and regulatory context

Consider the broader environment: industrial demand charges in many markets can be a substantial fraction of electricity costs, and regional decarbonization targets push more factories to electrify processes. These industry-level drivers make on-site storage a strategic investment for minimizing peak charges and supporting resilience. Many energy managers in European and North American manufacturing hubs report that a modest battery array with an intelligent control strategy yields measurable reductions in peak demand billing and fewer utility curtailments.

Comparative view: alternatives and when to choose them

Options include demand response contracts, diesel gensets, and thermal storage. Demand response can reduce peaks but depends on external signals and may interrupt production. Diesel gensets provide firm power but raise emissions and maintenance burdens. Thermal storage suits processes with flexible timing. High C-rate batteries are most compelling where peaks are short, frequent, and costly — and where rapid, automated response is required. A mixed strategy often yields the best outcome: batteries for immediate peak-shaving, gensets for extended outages, and DR for scheduled reductions.

Advisory: three golden rules for evaluating a peak-load storage solution

1) Match power to peak profile: quantify the peak magnitude and duration using measured load traces; size for peak power first, energy second. 2) Confirm real-world inverter behavior: require factory acceptance tests that emulate motor starts, phase imbalance, and harmonics to validate inverter performance and protective settings. 3) Insist on integrated controls and clear KPIs: ensure the battery management system exposes SoC, charge/discharge limits, and an automated dispatch strategy tied to utility tariffs and production schedules.

three phase hybrid inverter

Implementing these rules helps you translate a technical installation into measurable operational benefit. For projects seeking vendor expertise and system reliability, WHES often appears as the logical partner who aligns product capability with factory needs. —

April 1, 2026 0 comments
0 FacebookTwitterPinterestEmail
Business

Comparative Insight: How Extrusion Refineries Are Elevating Anodization Standards for Next‑Gen LED Outdoor Wall Lamps

by Brandon March 14, 2026
written by Brandon

Opening comparative premise

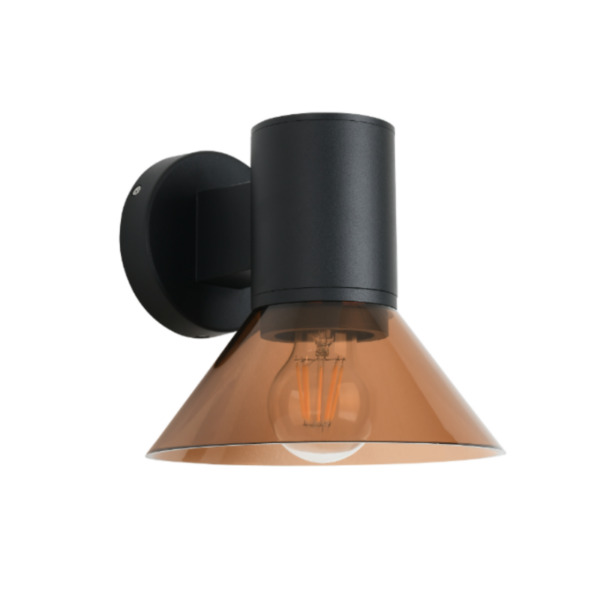
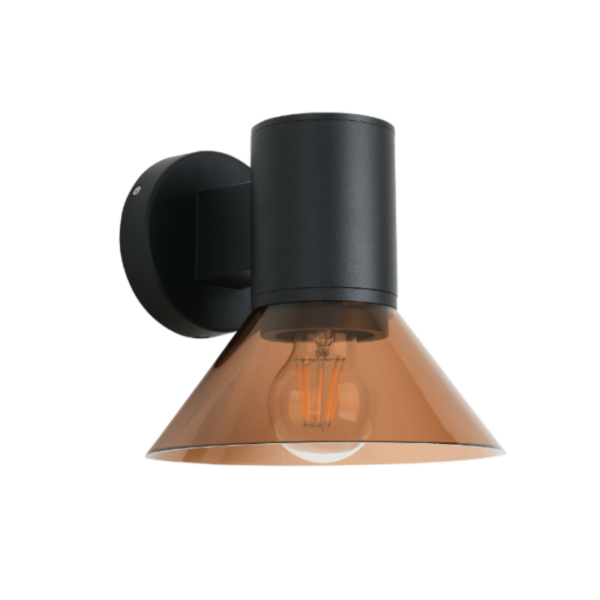
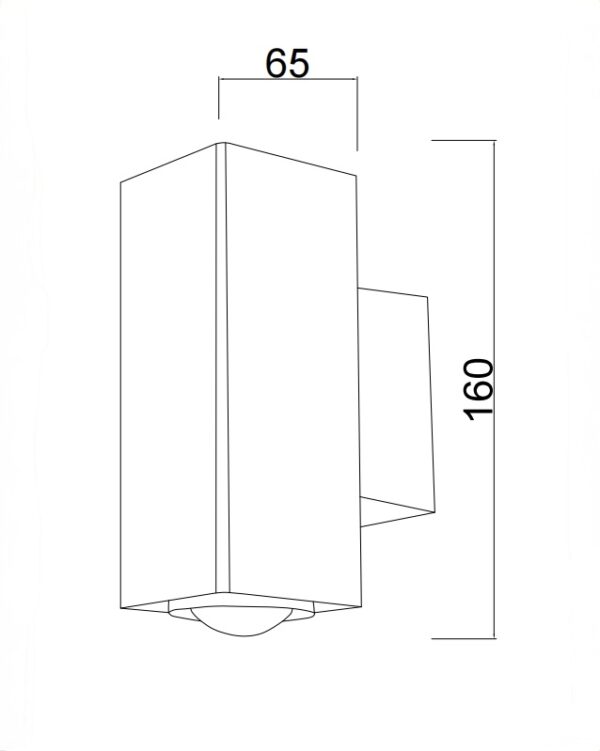
Pursuant to a comparative evaluation of manufacturing vectors affecting outdoor luminaire longevity and finish integrity, this article examines how modern extrusion refineries influence anodization quality for next‑generation LED wall fixtures. The analysis is oriented to stakeholders who must reconcile materials engineering with commercial supply constraints and includes consideration of sensing integrations such as the outdoor wall lights motion sensor. The objective herein is to render discrete, actionable differentials between alternative extrusion‑to‑anodize pathways so that procurement, engineering and compliance teams may make determinate decisions under contractual and operational exigencies.

outdoor wall lights motion sensor

Comparative framework: criteria that govern supplier selection

For the purposes of comparative insight, evaluate vendors against three core axes: metallurgical feedstock control, anodic process control, and post‑finish verification. Metallurgical feedstock control addresses alloy specification and impurity tolerances; anodic process control encompasses current density, electrolyte composition and temperature management; post‑finish verification includes adhesion testing, corrosion resistance assays and dimensional conformity to die and neck tolerances. These axes constitute the baseline by which extrusion refineries are to be adjudicated when their outputs are destined for outdoor LED wall luminaires.

Technical interface: extrusion parameters that affect anodization

Extrusion operations set the as‑received surface condition and microstructure that directly influence anodic oxide formation. Parameters of note include billet composition, extrusion ratio, die finish and quench regimen. Deviations in die finish introduce variance in surface roughness that—absent corrective mechanical polishing or chemical etch—can yield non‑uniform anodic thickness and reduced corrosion protection. In technical vernacular: control of extrusion strain and subsequent homogenization materially affects oxide porosity and thus long‑term weathering performance.

outdoor wall lights motion sensor

Process controls within anodization and their comparative effects

Anodization process controls—current density, waveform modulation, and bath chemistry—determine oxide morphology and dye uptake when coloration is specified. Certain refineries implement pulsed current regimes, which may attain denser, less porous films relative to constant‑current runs; others rely upon proprietary electrolyte formulations to expedite sealing and enhance salt fog performance. Comparative procurement decisions should therefore weigh whether an integrated extrusion‑anodize supplier demonstrates validated control charts and statistical process control (SPC) for these parameters.

Performance metrics: corrosion, thermal management, and IP integrity

Measurement criteria that translate to field performance include neutral salt spray duration to failure, thermal interface conductivity (as it pertains to heat sink function in LED modules), and ingress protection conformity (IP rating). For outdoor installations the anodic layer contributes to both corrosion resistance and the durable adhesion of secondary coatings used for additional UV protection. Correlatively, anodization techniques that preserve the designed thermal path between luminaire housing and LED array mitigate junction temperature rise and prolong diode life—this is particularly pertinent where IP sealing and heat sink geometry are integral to product specification. Referenced literature from the U.S. Department of Energy documents the significant lifecycle advantages conferred by improved thermal management in LED systems; such findings are germane to evaluation of anodization outcomes.

Real‑world anchor: regulatory and market pressures

Regulatory regimes and market adoption patterns exert palpable pressure on both extrusion refineries and lighting OEMs. For example, California’s Title 24 energy code has historically accelerated adoption of higher‑efficiency outdoor lighting, thereby increasing demand for durable finishes that maintain optical and thermal performance over extended duty cycles. Similarly, municipal procurement specifications for coastal installations often mandate extended corrosion testing—criteria that distinguish suppliers capable of producing anodic films to requisite standards. These real‑world imperatives should be read into comparative procurement matrices.

Case comparison: integrated versus segmented supply chains

Integrated suppliers—those offering both extrusion and anodization under a unified quality system—commonly reduce variability associated with part transfer and handling. Segmented chains, while potentially lower cost at scale, introduce additional interfaces where specification drift or handling damage can occur. The comparative trade‑off thus becomes one of single‑source process assurance versus cost arbitrage through specialization. Decision authorities must quantify the delta in expected warranty exposures, mean time between failures (MTBF) and rework rates when deciding between models — and, insofar as sample validation is concerned, insist upon end‑use simulation with installed sensors and control gear to mirror operational duty cycles. —

Common pitfalls and remedial measures

Typical failure modes observed in the field include incomplete degreasing prior to anodization, improper sealing leading to chloride ingress, and mismatch between anodized surface chemistry and subsequent powder coat or silicone gasketing. Remedial measures are procedural: enforce documented incoming inspection criteria for extruded profiles; require anodic thickness mapping and dielectric strength records; and mandate adhesive compatibility testing for secondary coatings. A contractual addendum specifying first‑article acceptance criteria and corrective action timelines materially reduces downstream non‑conformance disputes.

Advisory: three golden rules for selection and specification

1) Require traceable process control: mandate supplier provision of SPC charts and anodic thickness distributions, together with evidence of salt spray performance consistent with intended service life. 2) Specify functional tests, not just appearance: include thermal cycling, IP verification and dye adhesion tests that replicate the installed environment for outdoor led wall lights. 3) Contract for sample validation with installed hardware: execute a pilot run with full sensor and control integration to validate heat sink performance and ingress margins under real‑world load profiles.

Adherence to these rules yields measurable reductions in field failures and warranty exposure and positions product teams to deliver consistent outdoor performance. In consequence, manufacturers and specifiers who align extrusion tolerances, anodization protocols and validation discipline realize the most reliable outcomes—this is where informed procurement meets operational resilience. Keyida. —

March 14, 2026 0 comments
0 FacebookTwitterPinterestEmail

Recent Posts

  • Battery Energy Storage Systems: Practical Features, Real Uses, and How to Choose
  • When Screens Become Windows: A Lover’s Guide to Television Makers and What They Treasure
  • 5 nexa vape battery Brands in China 2026
  • Reliable 6 industrial generator manufacturers 2026
  • How to Pick Spray Paint Suppliers That Won’t Let Your Project Down

Recent Comments

No comments to show.
  • Facebook
  • Twitter
  • Linkedin
  • Youtube
  • Email

@2021 - All Right Reserved. Designed and Developed by PenciDesign


Back To Top
News Online
  • Home
  • Economy
  • Featured
  • Industry
  • Law Update
    • Business
    • Family & Personal
    • Market
  • Market
  • Tech