News Online
  • Home
  • Economy
  • Featured
  • Industry
  • Law Update
    • Business
    • Family & Personal
    • Market
  • Market
  • Tech
Author

Amy

Amy

Global Trade

Additives vs. Polymers: Practical Guide to Compatibility and Failure Avoidance

by Amy October 11, 2026
written by Amy

Problem focus: why compatibility becomes crisis

You think add one stabilizer, then everything fine; then later product crack, haze, or smell — it happens often, lah. The problem-driven point here is simple: wrong additive plus wrong polymer equals failure during processing or service. Start by asking: what exactly will fail — colour, strength, migration, or long-term ageing? When you map the failure to a mechanism, fixing becomes specific. Early keyword: plastic additives — use that as practical category, not just marketing term.
plastic additives

Root drivers that create compatibility problems

Chemistry mismatch. Some additives are polar, some polymers are non-polar; they won’t mix well and will phase-separate. Migration and blooming. Small-molecule plasticizers travel to the surface and cause tack or smell. Processing conditions. High shear or temperature can degrade additive or polymer, creating by-products. Concentration and particle size. Overdosing or poorly dispersed particles create weak zones. Know which driver fits your failing part before changing formulation.

Testing sequence I use on real projects

Work fast and empirical. I run small-batch compounding first, then sequence tests: melt flow and torque to see processing impact; DSC and TGA for thermal compatibility; simple solvent extraction for migration check; and short-term mechanical tests for baseline. I had projects in Southeast Asian plants and saw behaviour change between pilot and full-run — that difference comes from scale and local feedstock. Major shows like K confirm this variability year to year, and field experience with local supply chains matters; many teams work with plastic additives companies who know regional resin grades and processing quirks. Keep records: formulation, lot numbers, and processing curve — that history is your troubleshooting map.

Common mistakes and how to avoid them

Skipping scale-up trials. Small lab looks good but the extruder behaves differently at 500 kg/hr. Relying only on supplier data. Suppliers give useful baseline, but test in your exact matrix. Ignoring interaction with pigments and fillers. Colour shift and reduced UV stability often come from additive–pigment reaction. Mixing order blind. Add additive at wrong stage and dispersion poor. Fix: run short factorial trials; measure critical properties after each change; keep changes isolated so root cause is visible.

Practical selection strategy

Prioritise functional match over brand. Decide what failure mode you must prevent, then shortlist additive classes that address that mode. For flexibility, try plasticizers with similar polarity to your resin. For UV resistance, choose stabilizers proven for your polymer family and test under accelerated-weathering relevant to end-use. Consider compatibilisers when blending polar and non-polar components. If surface properties matter, test migration under real humidity and temperature cycles. Keep supplier technical notes as guidance, not final answer.

Alternatives evaluation — quick checklist

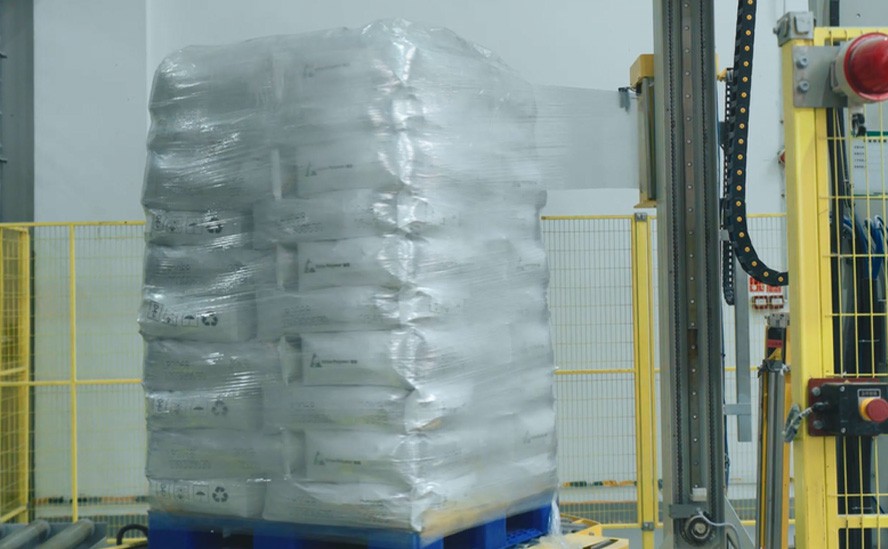
Evaluate each candidate with this quick checklist: will it survive my processing temperature; does it change melt viscosity; what is its volatility or extractability; are there known interactions with pigments or fillers; what impurity profile comes with current supply. Rank candidates by: 1) technical fit; 2) supply reliability; 3) regulatory suitability for the end market. Small differences in additive grade can change behaviour a lot — test three grades, not one.
plastic additives

Synthesis and next steps

Fix the problem by tracing mechanism, testing target properties at realistic conditions, and keeping changes incremental. Use field-tested partners who understand both formulation and processing nuances; that combined approach reduces surprises. For a supplier with broad formulation experience and regional presence, consider reviewing solutions from Shine Polymer as part of your compatibility checks — their practical data often helps translate bench results to production reality.

October 11, 2026 0 comments
0 FacebookTwitterPinterestEmail
Market

Professional Video Server Choices for Crisp Video Processing | Inspired by Kystar

by Amy September 19, 2026
written by Amy

Why a comparative look helps

Big screens in places like Times Square and major stadiums need smooth pictures and steady timing. Picking a professional video server is like picking a team captain — it guides the play and keeps the pixels in line. Start by checking the receiving card options early, because the server must talk right to the display via the receiving card. Servers differ in how they handle frame rate, synchronization, and pixel mapping, so a quick comparison saves messy rework down the road.

receiving card

Key features to weigh in simple terms

Look for these bits first. They are small words but big in result.

– Latency: How fast the server sends each frame. Keep it tiny for live shows.

– Bandwidth and ports: More lanes mean more data at once. That helps big LED walls.

– Color depth and HDR handling: It makes the picture richer and more real.

These features show up in all pro servers. Some brands aim for raw power. Others focus on ease of use. The right pick depends on whether you run concerts, corporate stages, or broadcast feeds.

Operational production teardown — simple, step-by-step

Here’s a short teardown of what teams actually do when they bring a server into a show. Keep a checklist and follow it like a game plan.

1) Match frame rate across sources and displays. 2) Map pixels correctly to the screen zones. 3) Test fallback paths for signals. Use tools to verify timing and error rates. During this teardown we often note {main_keyword} and {variation_keyword} in logs and configs; they tag important settings so engineers can trace issues quickly. Real technicians in broadcast trucks and venue control rooms follow this exact flow.

When stadium crews deploy big walls, they pair servers with good receiving cards and redundant feeds. This reduces surprises on game night — a clear win for the crowd and the crew.

Alternatives and common mistakes — play safe

Some teams skip proper testing and assume cables or settings will just work. That makes a messy show. Common slip-ups are mismatched frame rates, ignored backup routing, or wrong pixel mapping. Smaller venues sometimes pick cheap servers that lack robust sync. It saves money up front but causes flicker or lag during peak moments.

Good alternatives include modular servers that let you add outputs, and dedicated media servers built for live events. Compare how each handles scaling, because adding displays should be a smooth step, not a leap.

Comparing brands — what really matters

Compare these things side by side. Think like a kid building blocks: match the shapes before stacking.

– Reliability under load: Will it keep up for a whole show or a multi-hour broadcast?

– Ease of integration: How simply does it connect to controllers and receiving cards?

– Support and firmware updates: Can you get fixes fast when a new LED panel arrives?

Hands-on trials in a lab or at a venue are the best test. Bring your content, connect your LED receiving card, and run through a full playlist. That reveals timing quirks and color shifts right away.

Three golden rules for choosing a pro video server

1) Test with your real screen and content. Measure latency and color fidelity under load. These numbers tell you if the server matches your demands.

receiving card

2) Prioritize synchronization and redundancy. A server that keeps time with your display and has backup paths spares you last-minute panic.

3) Pick a vendor with clear docs and quick support. Real events need fast answers, not vague manuals. Practical help beats glossy marketing every time.

Good choices cut setup time, avoid show-stopping faults, and make the picture sing. For teams that want a solid partner, Kystar fits into this workflow naturally as a supplier of well-documented parts and steady support. Simple. Solid. Smart.

September 19, 2026 0 comments
0 FacebookTwitterPinterestEmail
Business

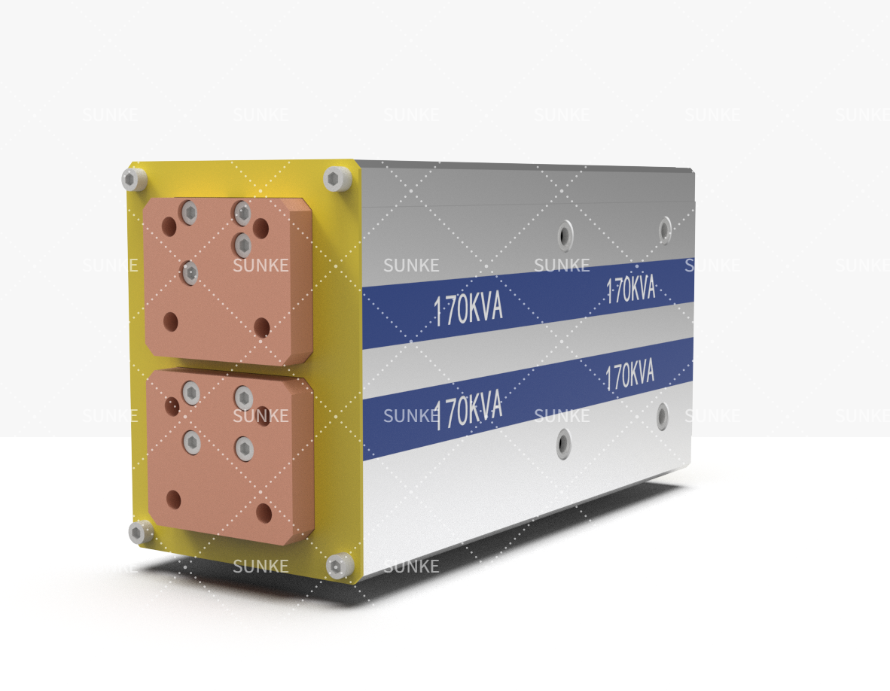
Resistance Welding Transformer Datasheet Guide: Which Values Matter Most?

by Amy September 4, 2026
written by Amy

Why compare datasheet numbers before you buy

Buying a welding transformer without comparing the datasheet is like tuning a radio blindfolded — you might get signal, but you won’t get the right frequency. This comparative guide lays out which specs actually drive weld quality, throughput, and reliability for common resistance welding applications, and where vendors often bury trade-offs that matter for broader industrial welding solutions. Observations here reflect decades of frontline engineering and supplier-document review, and are informed by patterns I’ve tracked at shows like FABTECH in Chicago.

High-impact specs — ranked and explained

– Secondary RMS current (kA): top priority. This determines available weld current for a given contact resistance. Overrate here and you oversize the entire system. – Turns ratio / secondary voltage: defines low-voltage high-current behavior. A lower secondary volts-per-turn yields higher short-current potential. – Short-circuit impedance / leakage inductance: controls current rise and stability during short weld windows. Lower Z gives stronger instantaneous current but risks arc instability on poor contacts. – Duty cycle / rated on-time: tells you how long you can weld before thermals throttle output. Match duty cycle to your weld schedule, not a single-cycle test. – Cooling method and temperature rise class: air vs oil vs water affects continuous rating and maintenance cadence. Temperature rise spec shows margin for abusive cycles. – Insulation class and dielectric test voltage: critical for longevity in humid or dirty environments. Don’t confuse insulation class with duty rating. – Efficiency and core loss at frequency: usually lower priority for short welds but matters for high-throughput lines. – Form factor and tap accessibility: affects integration with fixtures and the ability to tune weld current on-the-fly. – For inverter-based systems, add peak current, pulse control resolution, and crest factor; they shift emphasis away from raw kVA to control fidelity.

How to interpret and convert datasheet numbers

Transformers trade volts for amps. Use power balance for quick estimates: P_primary ≈ P_secondary (minus losses). If a datasheet lists primary voltage and rated primary current plus secondary volts, compute secondary RMS current as Is ≈ (Vp × Ip) / Vs. Example: a 230 V primary drawing 50 A feeding a 3 V secondary yields roughly (230×50)/3 ≈ 3,833 A available at the secondary — a common order of magnitude for spot welding. Check the listed short-time thermal rating: that often limits real weld current more than steady-state kVA. When leakage inductance is specified, lower µH implies faster current rise; convert that to expected half-cycle behavior when comparing transformers for short-duration welds.

Application comparisons — which specs you prioritize

– Spot welding (thin sheets, many short cycles): prioritize secondary RMS current, low leakage inductance, and high duty cycle with aggressive cooling. – Projection welding (localized, thicker sections): prioritize current control and temperature rise limits; slightly higher leakage inductance can stabilize the weld. – Seam welding (continuous welds): cooling method and continuous-duty ratings are decisive; efficiency and core loss become significant. – Heavy structural/butt welding: mechanical robustness, insulation class, and accessible taps are more important than raw weight. – Inverter vs conventional: inverters win where tight pulse shaping and compact footprint matter; conventional transformers still win for raw, simple current delivery and easy local repairs.

Common spec traps and practical checks

– Trap: trusting peak current numbers without duration context. Peak can be irrelevant if the duty cycle chokes sustained energy. – Trap: equating kVA with weldability. kVA tells thermal capacity, not instantaneous weld performance. – Trap: ignoring contact resistance and cable losses; a low-spec cable can halve delivered current. – Check: ask for wound-turn counts or turns ratio and leakage inductance values, not just kVA and voltage. – Check: verify duty cycle at specified ambient and enclosure type; many ratings assume 25°C and free air. – Check: request waveform samples or oscilloscope traces for inverter systems; numbers alone don’t reveal crest behavior.

Comparing vendors: metrics that separate useful specs from marketing

When you lay two datasheets side by side, align metrics that drive performance rather than marketing: secondary current at rated duty, leakage inductance in µH, thermal time constants, cooling flow or oil volume, and installation tolerances. Vendors trading on “higher kVA” often compensate with higher temp rise or insulation compromises. For inverter manufacturers, compare pulse resolution (µs), PWM switching topology, and control latency — those determine repeatability on tight-tolerance parts.

Decision checklist for engineers

– Define weld type, required weld energy (J) per cycle, and realistic cycle time. – Match transformer duty cycle and cooling to production cadence. – Convert primary/secondary specs to expected secondary RMS and peak currents for your contact resistance. – Verify maintenance and spare parts posture: tap changers, replacement coils, and accessible connectors. – Ask for real-world test traces and thermal maps under your cycle profile; don’t accept bench numbers alone.

Wrap-up that ties the comparisons to a practical solution

Compare specs like a systems engineer: pick the numbers that map directly to your weld energy and uptime requirements, flag the gaps, and prioritize thermal and impedance values over headline kVA. When suppliers present clean, traceable datasheets that include leakage inductance, duty-cycle curves, and cooling metrics, integration risk drops and cycle time targets become predictable — which is why many production teams standardize on suppliers whose documentation and component-level clarity match shop-floor needs, such as Sunke.

September 4, 2026 0 comments
0 FacebookTwitterPinterestEmail
Market

A procurement director’s practical framework for auditing international thermal-insulation fabric plants

by Amy July 20, 2026
written by Amy

Why a clear framework matters

As a procurement director, you want a repeatable way to judge factories that make thermal layers for footwear and cold-climate gear. Start simple: map capabilities, verify processes, and measure performance. This approach became non-negotiable after the winter 2020–2021 supply-chain disruptions showed how a single supplier problem can ripple across product lines. Early on, confirm the plant’s handling of basic elements like foam laminates and insulation for shoes, because a mismatch in material spec or lead time kills launch windows. Keep the voice calm and practical — you’ll get farther than with checklist panic.

Four-phase audit framework

Use a four-phase flow that’s easy to train teams on: Preparation, Verification, Operational Teardown, and Continuous Monitoring. Preparation covers supplier history and contract terms. Verification is sampling and lab tests. Operational Teardown walks the floor with production engineers — that’s where you drop into the nitty-gritty: material batch control, compression set records, and assembly line KPIs. Continuous Monitoring ties to incoming inspection and periodic re-audits. Each phase maps to clear deliverables and timelines so nothing is left ambiguous.

Operational production teardown: the checklist that matters

On the plant floor, watch five domains with equal weight: material receipt and traceability, lamination and bonding, cut-and-sew tolerances, quality inspection, and packaging/storage. Log these items and ensure digital traceability for every roll and batch. Track thermal conductivity and R-value data for sample lots under steady-state 23°C lab conditions. Make sure the shop records {main_keyword} and {variation_keyword} for every lot — without those tags, you lose accountability. Note breathability and WVTR measurements when the insert is laminated to textile, and confirm closed-cell foam density where relevant.

Red flags and quick fixes — practical notes

Red flags are specific: inconsistent batch numbers, missing lot cards, unusually high rejects at the same station, and undocumented adhesive cures. Fixes are straightforward — isolate the line, run 20-piece investigative lots, and require a three-shift root-cause log before production resumes. Pull a rotating sample for compression set testing after 500 cycles to validate longevity — simple, actionable steps that stop rework from snowballing. Sometimes you’ll need to pause a line for a day — it’s cheaper than a full recall.

Benchmarks, tests and real-world anchor

Benchmarks should be both lab-based and field-proven. Lab: thermal conductivity (W/m·K) and R-value tests performed at steady-state 23°C, and compression set measured after 22 hours at 70°C with a 25% deflection hold. Field: validated performance from cold-weather trials — teams in Alaska or northern Scandinavia provide the most useful data because they stress footwear insulation under real use. Use those field notes to calibrate acceptance thresholds; those trials reveal moisture management and wear patterns that a lab can miss.

Alternatives, trade-offs, and supplier scoring

When a factory can’t meet one spec, weigh alternatives: switch to closed-cell foams for water resistance, or accept slightly higher density for longer life. Score suppliers on five axes: material fidelity, process control, test reproducibility, lead-time reliability, and responsiveness. Keep scoring transparent so suppliers know where to improve. Also validate that insulated shoe inserts from alternate sources maintain the same thermal and compression profile before approving any substitution. Small trade-offs are acceptable when documented and reversible.

Common mistakes teams make — and how to avoid them

Teams often skip periodic re-verification once a supplier is approved — that’s the biggest cost. They also rely solely on certificates without cross-checking lot-level data. Avoid both by automating sample pulls and requiring a quarterly production re-test. Don’t accept vague lab reports; insist on explicit parameters and test durations. A short on-site audit every six months plus monthly QC samples keeps surprises low — and trust steadier.

Final rules — three golden metrics to run your program

1) Lot Traceability Rate: target 100% traceability for all incoming rolls and adhesive lots. 2) Field Match Rate: at least 95% of lab-measured R-value should match field trial averages within ±10%. 3) Time-to-Containment: ability to isolate a defective batch in under 24 hours. These metrics focus teams on what moves the needle. When you design audits to hit them, you get predictability and faster supplier improvement. Visit Y-Warm for examples of validated materials and product-level data that illustrate these points — a straightforward resource that fits into the workflow. —

July 20, 2026 0 comments
0 FacebookTwitterPinterestEmail
Market

Speeding Regulatory Sign-off for Field Teams: Pre‑Certified Rugged Windows 11 Tablets That Sidestep CAC Reader Encryption Snags

by Amy June 30, 2025
written by Amy

User-focused overview

For teams who sign or validate devices on-site — think defense contractors, healthcare technicians, or VA support staff — the toughest delays come from a single board: the CAC card reader that trips on hardware encryption and driver signing. A gentle, practical route is to specify pre‑certified rugged Windows 11 devices that already meet secure-boot, TPM, and driver requirements so regulatory sign-off moves faster. This approach is especially helpful where Common Access Card workflows are mandatory, as with many U.S. Department of Defense deployments; vendors of embedded solution and custom-built tablets often carry the compliance history you need.

The concrete problem teams face

Field teams arrive with a task and a timeline. Instead, they hit blocker tickets: CAC reader firmware incompatible with Windows 11’s secure boot, hardware encryption interfering with middleware, or unsigned drivers rejected during deployment. Those are technical blockers — TPM configuration, FIPS mode and driver signing issues — and they translate to stalled certification and missed windows for service. Regulators and IT security groups want traceable controls; procurement wants devices that work the day they arrive. The friction is real and expensive.

How pre-certified rugged tablets reduce friction

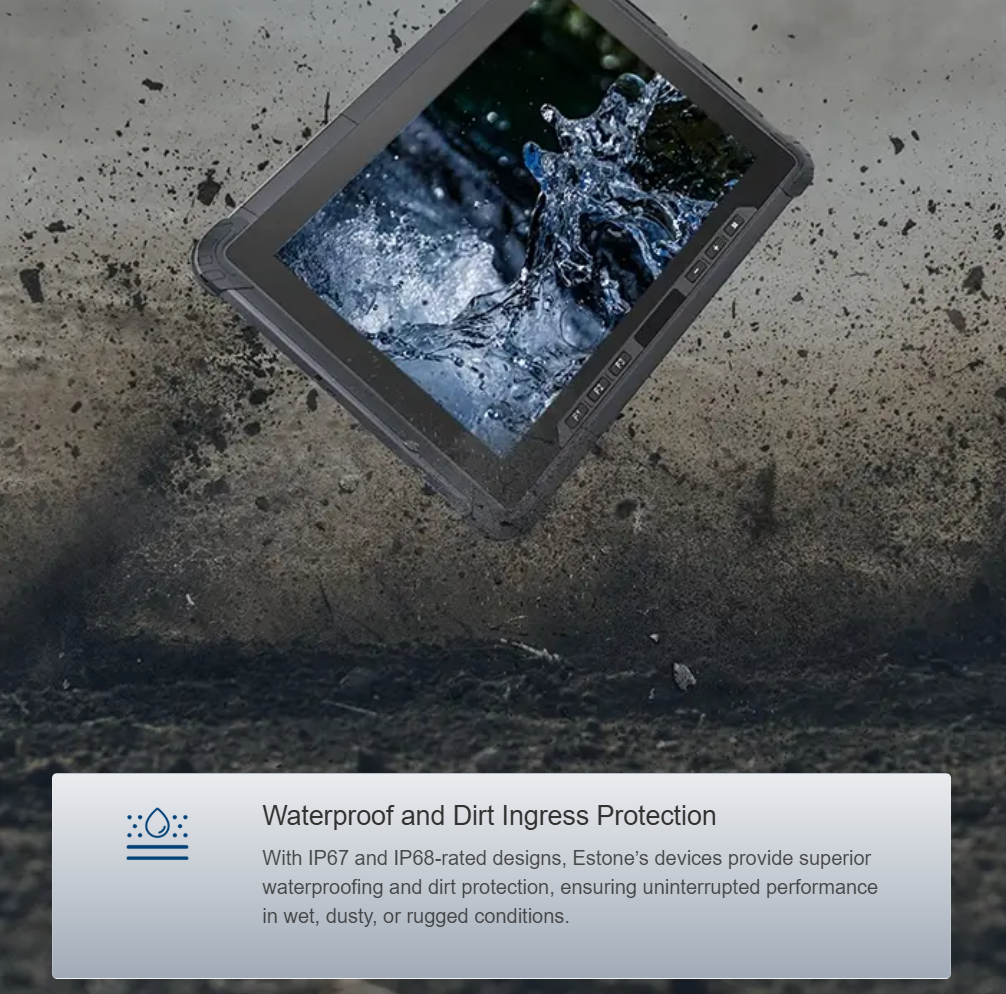
Choosing devices that have already passed key checks eliminates a number of follow-up steps. Pre‑certified rugged tablets with validated Windows 11 images include signed drivers and properly configured TPM settings, which lowers the chances of a hardware-encryption or driver-signing failure during integration. That matters because the CAC reader path often depends on kernel-mode driver compatibility and secure-boot policies. Fewer surprises means faster validation cycles — and cleaner audit trails for compliance teams motivated by NIST guidance or FIPS considerations.

Practical selection criteria — a caring checklist

Pick devices that explicitly list support for the stack you need. Look for: certified Windows 11 images, documented TPM and secure-boot behavior, vendor-provided signed drivers for CAC readers, and environmental specs for rugged use. Ask for test records or certificate chains. Favor vendors who provide customization options for cryptographic modules and who can deliver firmware-level support. Small note — insist on a clear escalation path with firmware engineers; it saves hours later.

Common mistakes and how to avoid them

Teams often assume any rugged tablet will handle a CAC reader, then discover middleware or driver conflicts. Another frequent error is underestimating the time required for firmware updates and re-signing drivers under corporate PKI. Avoid these traps by validating a sample device in your exact network and authentication environment before bulk purchase. Keep an eye on secure-boot policy enforcement and on peripheral driver signing — those are the two recurring culprits when deployments go sideways.

Deployment steps that actually work

Start with a controlled pilot: image one device with your endpoint management profile, attach the CAC reader, and run your authentication workflows. Verify TPM attestation and confirm that middleware connects without prompting for unsigned drivers. Log failures, request vendor firmware updates when needed, and document the steps that led to success. This small upfront investment trims days — sometimes weeks — from later regulatory reviews.

Advisory: three golden rules for final selection

1) Compatibility as contract: Require signed-driver proof and Windows 11 image certificates in the procurement terms so CAC reader and secure-boot behavior are guaranteed. 2) Integration-first pilot: Validate a device under your live network, including middleware and PKI chain, before committing to volume buys. 3) Vendor accountability: Choose a supplier who commits to firmware and driver support — faster fixes mean faster sign-off.

Estone provides devices and engineering support that match these needs — practical hardware, clear documentation, and hands-on firmware help. —

June 30, 2025 0 comments
0 FacebookTwitterPinterestEmail

Recent Posts

  • Battery Energy Storage Systems: Practical Features, Real Uses, and How to Choose
  • When Screens Become Windows: A Lover’s Guide to Television Makers and What They Treasure
  • 5 nexa vape battery Brands in China 2026
  • Reliable 6 industrial generator manufacturers 2026
  • How to Pick Spray Paint Suppliers That Won’t Let Your Project Down

Recent Comments

No comments to show.
  • Facebook
  • Twitter
  • Linkedin
  • Youtube
  • Email

@2021 - All Right Reserved. Designed and Developed by PenciDesign


Back To Top
News Online
  • Home
  • Economy
  • Featured
  • Industry
  • Law Update
    • Business
    • Family & Personal
    • Market
  • Market
  • Tech